Engineered Stone Cladding Systems for Commercial & Residential Projects
As a leading global OEM/ODM manufacturer and exporter, we integrate advanced material science with artisanal stonemasonry. From lightweight polyurethane (PU) artificial rock panels to sintered stone mega-slabs and natural stacked slate ledger tiles, our factory-direct cladding solutions empower specifiers, architects, and wholesalers worldwide.
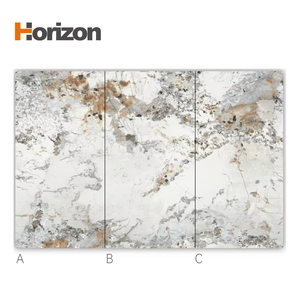
Multicolored Sintered Stone Slab Granite Design
Ultra-compact 12mm/20mm sintered porcelain slabs with high-definition granite veining. Zero porosity, scratch-resistant, UV-proof engineered stone ideal for high-traffic feature walls, kitchen islands, and exterior ventilated facade cladding.
Inquire Now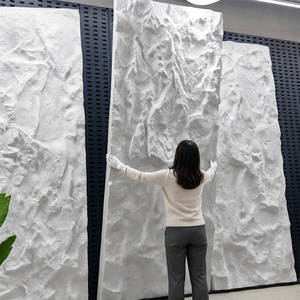
Waterproof PU Cultured Stone 3D Wall Panel Board
High-density polyurethane artificial rock veneer mimicking natural slate textures. Ultra-lightweight (4kg/m²), fully waterproof, moisture-resistant, and flame-retardant. Perfect for rapid structural installation on exterior facades and indoor features.
Inquire Now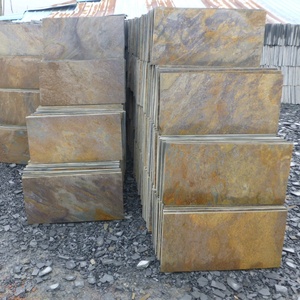
Outdoor Mixed Rusty Beige Slate Natural Stone Tile
Authentic split-face natural slate wall cladding tiles. Features rich iron-oxide tone variations, exceptional weatherability, anti-freeze endurance, and thermal inertia for outdoor patio walls, landscape features, and architectural siding.
Inquire Now
CE Certified Polyurethane Faux Natural Stone Board
Commercial-grade exterior faux natural stone siding tested to European safety standards. Features molded structural interlocking edges for seamless joint installation, high thermal insulation value, and superior UV color-fastness.
Inquire Now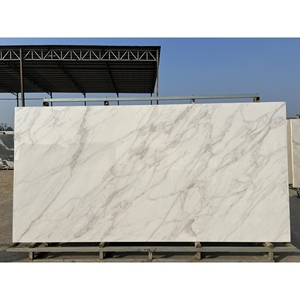
Customized Engineered Marble Surface Sintered Slab
Custom OEM/ODM engineered marble-effect sintered slabs. Formulated with mineral aggregates under 30,000-ton hydraulic compaction, delivering continuous book-matched veining, acid stain resistance, and high flexural strength for luxury wall features.
Inquire Now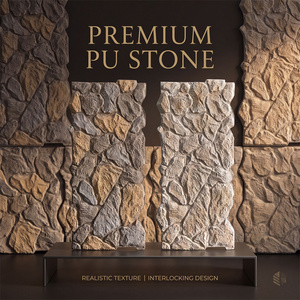
LONGTE Textured Rock Effect PU Faux Exterior Siding
Precision-molded polyurethane rock effect panels engineered for rapid screw-fixed installation without wet mortar. Integrated insulation backing reduces thermal bridging, providing a lightweight, low-maintenance architectural facade.
Inquire Now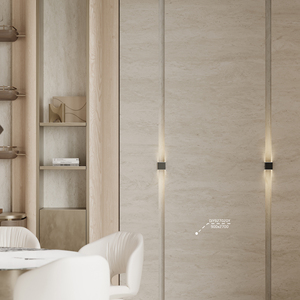
Matte White Sintered Stone Slabs 900x2700mm
Floor-to-ceiling 900x2700mm soft-touch matte white sintered stone. Features thermal shock resistance up to 1200°C, zero VOC emissions, and extreme dimensional stability. Engineered for modern minimalist residential and hospitality interiors.
Inquire Now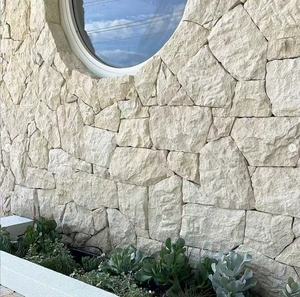
Stacked Random White Limestone Ledger Wall Cladding
Hand-crafted random white limestone stacked ledger stone panels. Offers deep 3D tactile relief, natural light diffusion, and extreme weather durability for commercial building entrances, boundary walls, and fireplace surrounds.
Inquire NowIntegrated OEM/ODM Engineering: From Concept Renderings to Installed Facades
In high-end architectural sourcing, stone cladding is never merely a decorative skin—it is a critical building envelope component requiring precise mechanical performance, fire compliance, and weatherability. Our integrated manufacturing eco-system Bridges the gap between architectural creative vision and scalable industrial production.
In-House Tooling & Mold Design
We operate proprietary CNC mold machining and custom silicone casting centers. For custom ODM orders, we translate CAD files into sub-millimeter precision PU foam molds and sintered slab pressing dies in under 10 business days.
Design-For-Manufacturability (DFM)
Our engineering department reviews site anchoring plans, wind-load requirements, structural deadweight constraints, and thermal expansion joints, optimizing stone panel thickness and backing geometry before production commences.
Rigor Quality Assurance (QA/QC)
Every production batch undergoes spectrophotometer color matching, ultrasonic internal flaw detection, flexural modulus testing (ASTM C880), and water absorption verification (ASTM C97) to guarantee zero field failures.
With global project hubs operating across Toronto, Miami, Lisbon, Riyadh, and Dubai, our specialized technical teams handle shop drawing approvals, custom material sampling, export packing, and cross-border logistics to keep major architectural projects on schedule and under budget.
Macro Development Trends Shaping Architectural Stone Cladding
Driven by strict urban sustainability codes, rising labor costs, and evolving aesthetic demands, the global architectural wall cladding market is experiencing a profound technological transformation. Our R&D divisions remain at the forefront of these structural shifts:
1. The Rise of Ultra-Compact Sintered Stone Facades
Traditional thick stone slabs (20mm–30mm) impose massive dead loads on structural steel frames, necessitating expensive heavy-duty anchoring systems. Sintered stone technology utilizes natural clays, feldspars, and quartz oxides compressed at extreme pressures (>400 bar) and fired in kilns above 1200°C. The resulting material exhibits near-zero water absorption (<0.05%), complete frost resistance, and exceptional flexural strength in thin 6mm and 12mm profiles, making it the preferred choice for modern rainscreen facades.
2. Polyurethane (PU) Artificial Rock Revolution
High-density structural polyurethane (PU) formulations have revolutionized interior and exterior wall renovation. By combining elastomeric resin matrices with fire-retardant blowing agents, PU cladding panels capture the intricate organic textures of natural split slate and stacked ledge rock at 80% less weight than real stone. This lightweight profile eliminates the need for structural wall reinforcement and specialized stonemasons, lowering installed labor costs by up to 60%.
3. Translucency and Integrated LED Backlighting
Modern commercial design increasingly integrates dynamic lighting directly into the structural stone envelope. Advanced composite techniques now combine ultra-thin natural quartzite or sintered stone veneers with glass/acrylic polymer substrates. This enables uniform light transmission for hotel reception backdrops, bar fronts, and illuminated exterior building features without compromising panel rigidity.
| Material Category | Avg Density (kg/m²) | Water Absorption | Fire Rating Class | Installation Method | Primary B2B Application |
|---|---|---|---|---|---|
| Sintered Stone Slabs | 15 - 30 kg/m² | < 0.05% | Class A1 (Incombustible) | Rainscreen / Structural Adhesive | High-rise Facades, Luxury Interiors |
| PU Cultured Stone | 3.5 - 5.0 kg/m² | < 0.10% | B1 / Class 1 Flame Retardant | Direct Mechanical Screw-Fixed | Rapid Retrofits, Commercial Retail |
| Natural Stacked Slate | 45 - 65 kg/m² | 0.5% - 1.5% | Class A1 (Incombustible) | Wet Mortar / Anchored Ledge | Landscape Architecture, Villa Exterior |
| Engineered Marble | 30 - 45 kg/m² | < 0.30% | Class B1 / A2 Option | Dry-Hang Metal Clip System | Hotel Lobbies, Commercial Interiors |
Future Sourcing Trends for Buyers, Exporters, and Wholesalers
In an increasingly complex global trade environment, procurement officers, real estate developers, and international importers must navigate shifting supply dynamics. Key procurement benchmarks include:
BIM LOD 350 / 400 Digital Submittals
Modern tier-1 general contractors require suppliers to provide fully parametric Building Information Modeling (BIM) objects. We supply LOD 350-compliant BIM assets containing complete material metadata, thermal resistance values (R-value), expansion coefficients, and anchoring point vectors, ensuring seamless digital twin integration during project engineering.
Decarbonization & EPD Environmental Declarations
Green building certifications such as LEED v4.1 and BREEAM dictate strict carbon limits for building envelopes. Sourcing stone cladding from factories equipped with closed-loop water recycling systems, solar kiln heating, and low-embodied-carbon PU matrices allows project specifiers to gain essential points under Materials and Resources (MR) credits.
Modular Off-Site Assembly & Rainscreen Dry-Hang Systems
On-site labor scarcity has accelerated the shift toward off-site modular construction. Stone cladding is increasingly procured as pre-assembled curtain wall panels or interlocking dry-hang rainscreen systems. By eliminating wet mortar installation on site, project developers drastically reduce construction timelines while eliminating efflorescence risk caused by cement moisture migration.
Frequently Asked Questions (B2B Procurement & Engineering)
What are the key technical differences between PU cultured stone and natural slate cladding?
How do you ensure color consistency across large batch OEM/ODM orders?
Can your stone cladding panels withstand extreme freeze-thaw cycles and UV exposure?
What minimum order quantities (MOQ) and lead times apply for custom ODM mold designs?
How are stone cladding products packaged to prevent damage during international ocean freight?
What structural mounting systems are recommended for exterior high-rise cladding?
Do your stone cladding products meet international fire safety regulations?
Do you offer CAD engineering, shop drawings, and installation support for architectural projects?
Partner with a World-Class OEM/ODM Stone Cladding Exporter
Whether you require custom PU rock mold development, large-format sintered stone mega-slabs, or mixed natural slate containers, our global engineering team is ready to support your technical specification.